Custom Machined Plastic Parts for the Energy Industry
Great Plastics manufactures custom engineering plastic components to customer drawings for energy equipment and industrial systems. Material selection and machining requirements are reviewed against operating temperature, mechanical loads, wear, chemical exposure and dimensional requirements.
solutions
Plastic Components for Energy Equipment
Source oil and gas plastic components for fluid control, rotating equipment and electrical assemblies. Specify the fluid, motion and electrical duty behind each part.
Valve Seats & Sealing Parts
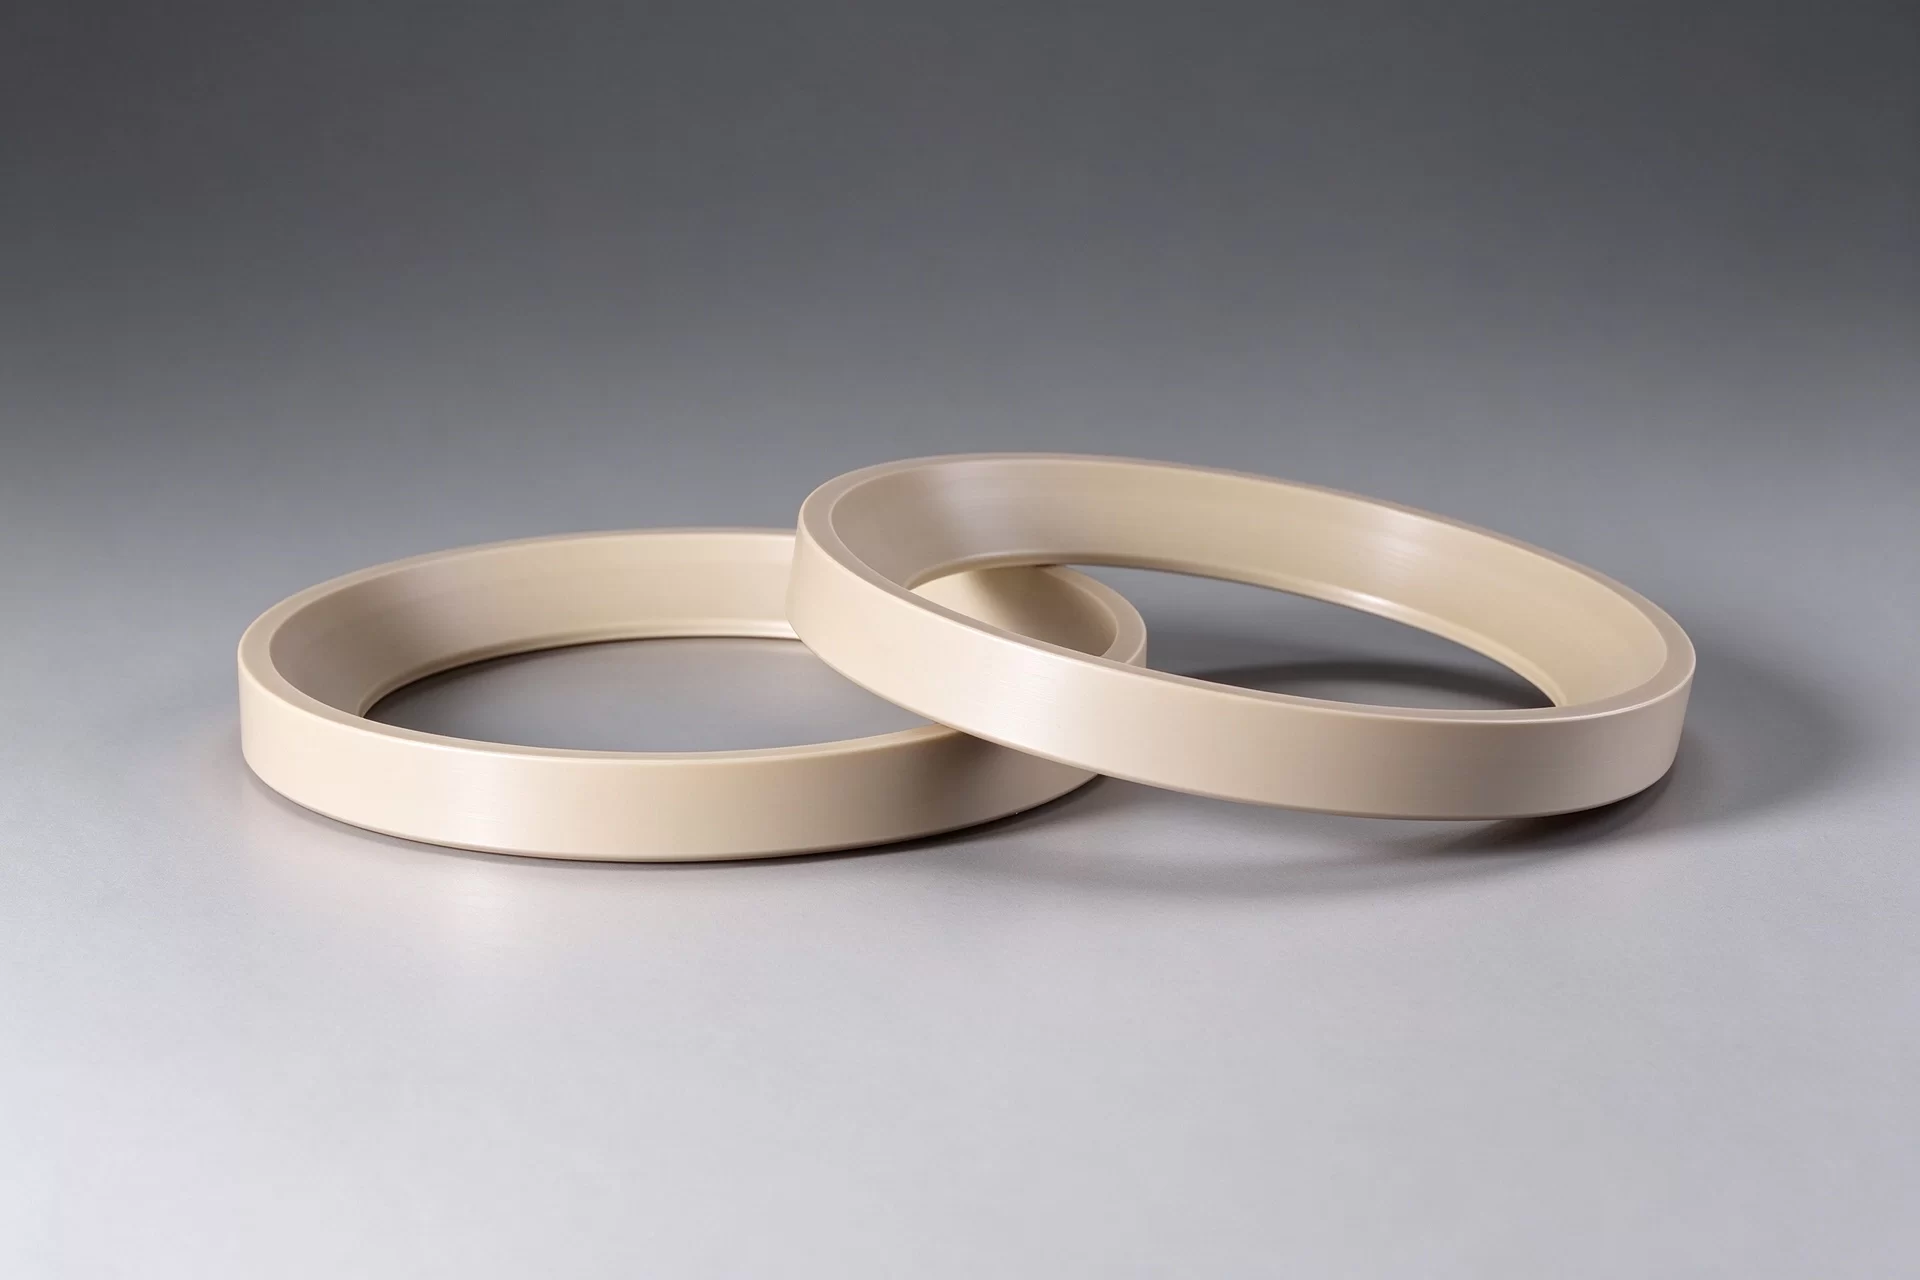
PEEK valve seats, backup rings and stem guides made to your drawing. The sealing profile must hold under compression while resisting the process fluid. Grade choice also affects creep, contact wear and the finish at the sealing interface.
Bushings, Sleeves & Wear Rings
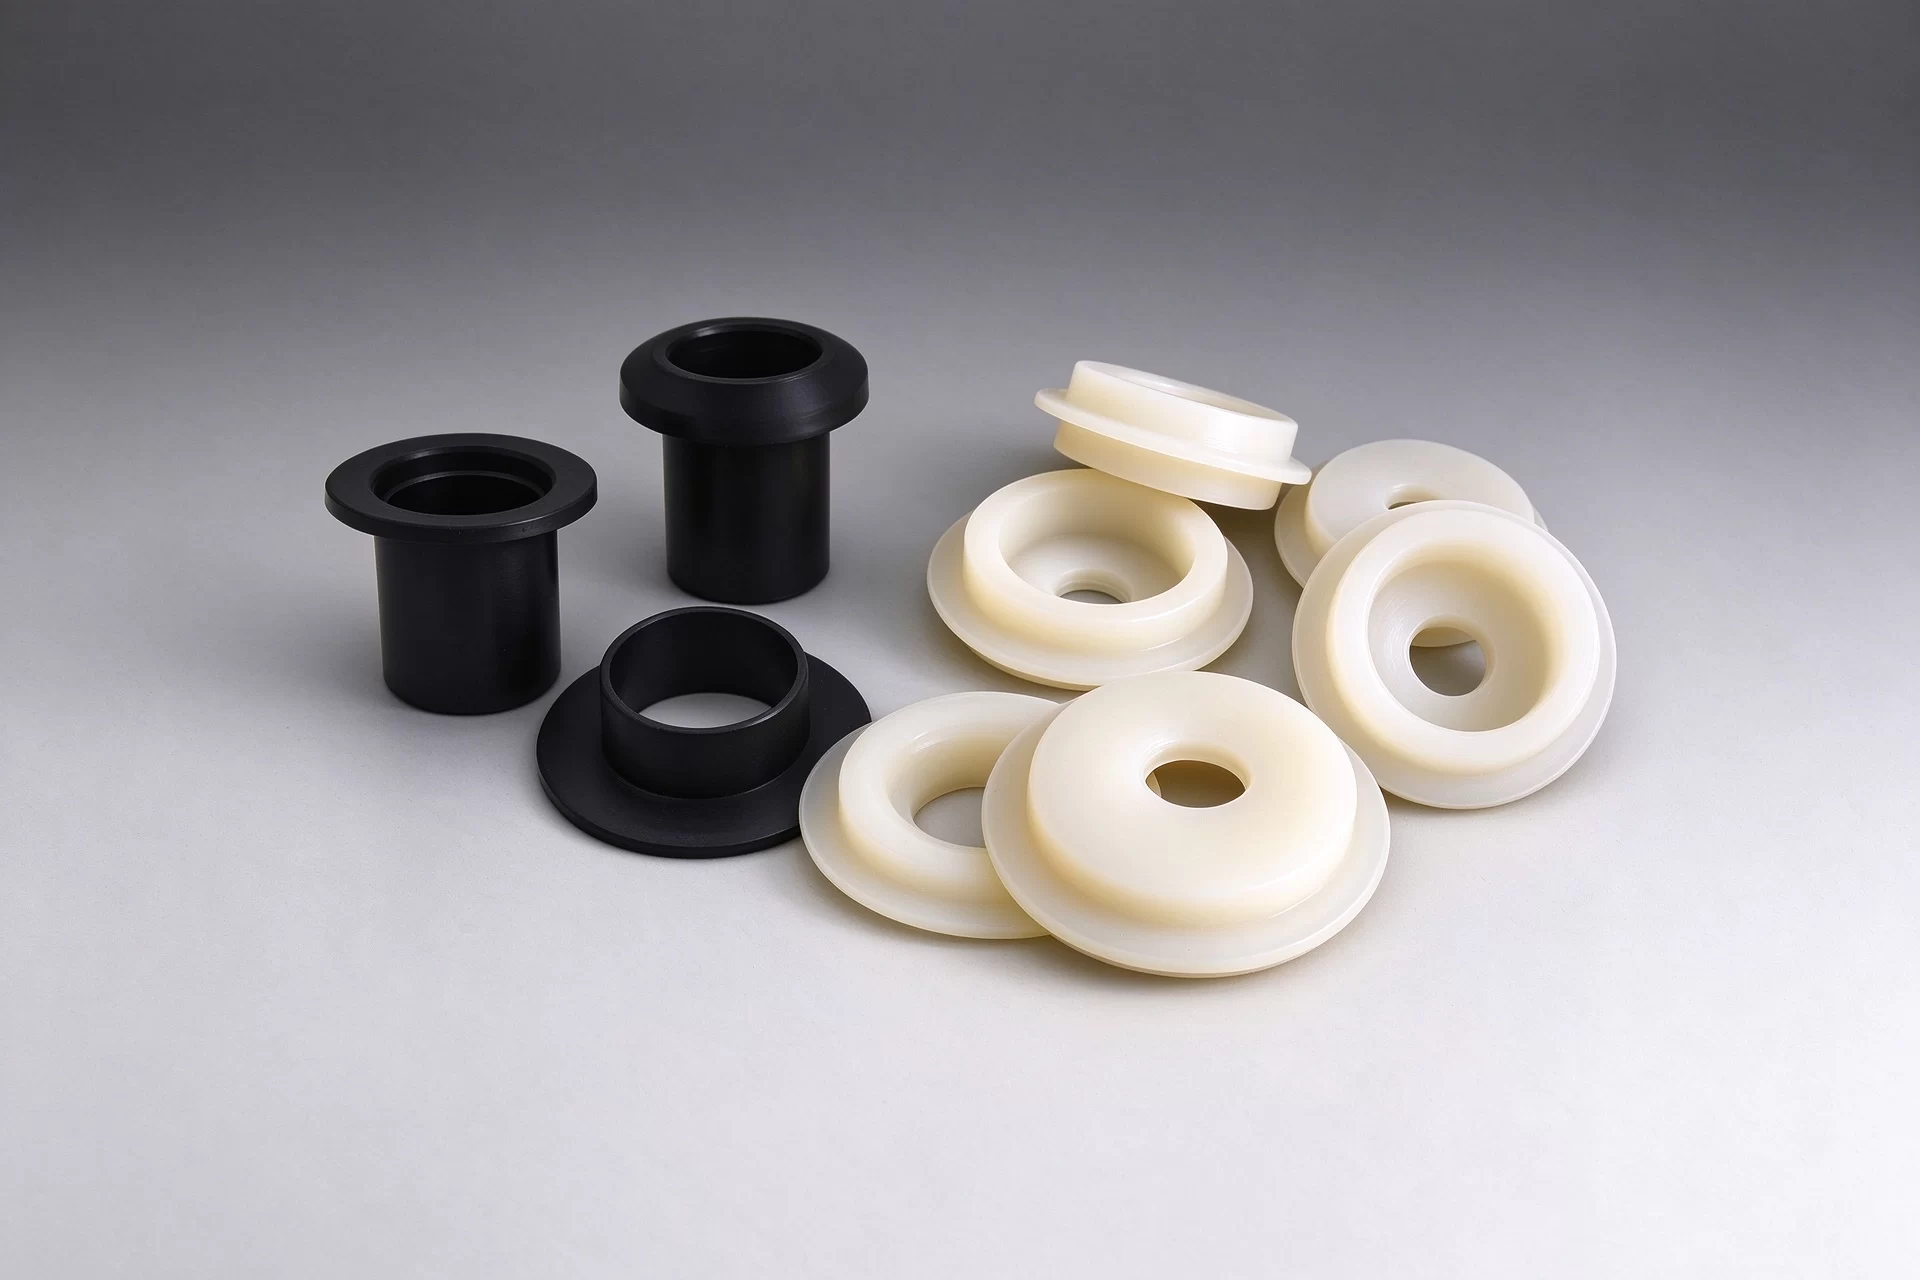
Components for shaft guidance, sliding contact and running clearances in pumps and rotating equipment. PEEK, PPS and PAI offer different load and wear options. Abrasive particles, dry running and the mating surface can change the grade choice.
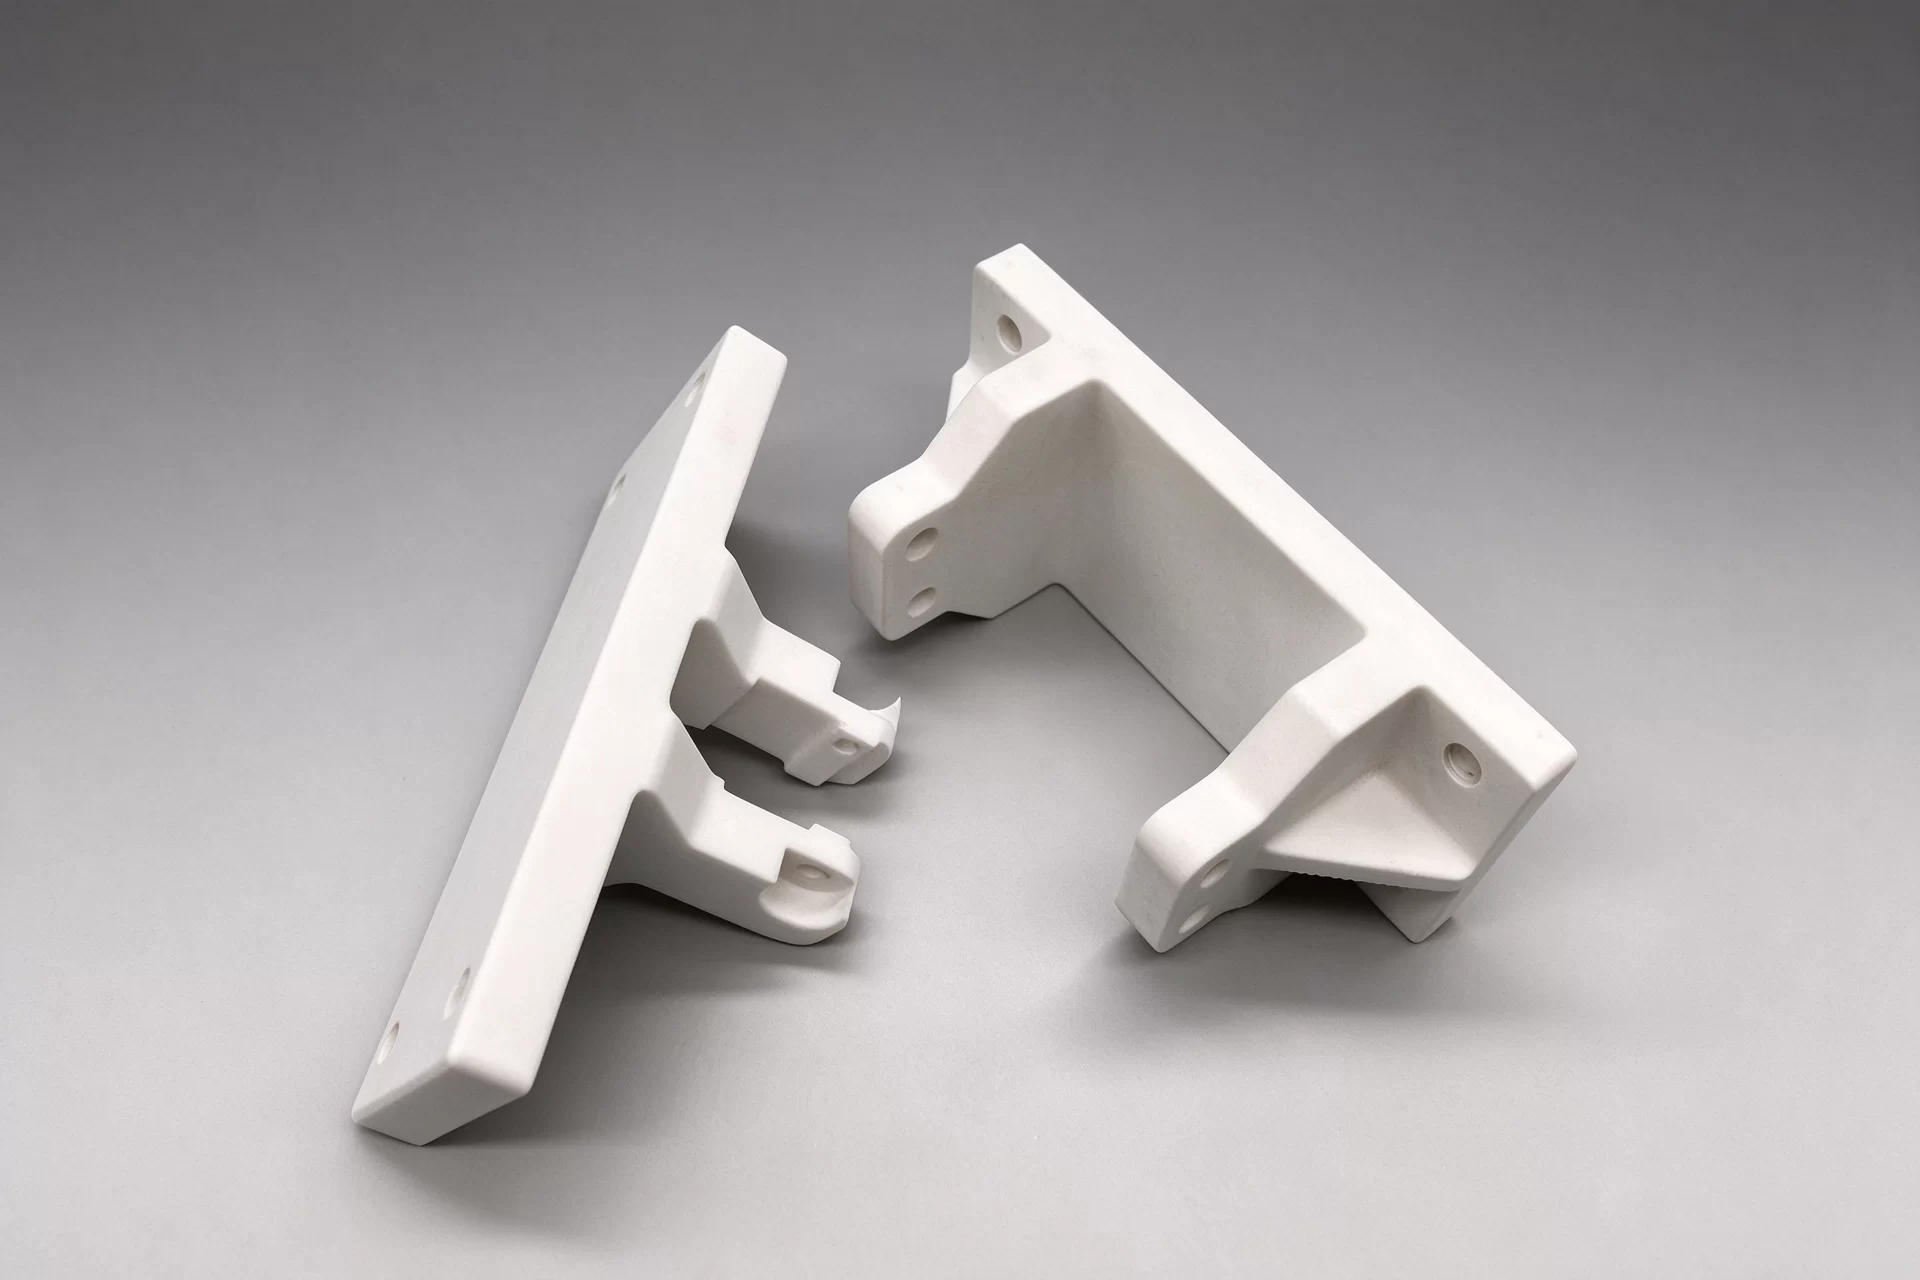
Electrical Insulators & Supports
Connector bodies, pin carriers, spacers and equipment supports in PEEK, PEI, PPS or PI. Pin spacing, wall sections and mounting holes matter alongside dielectric performance. Conductive fillers require a different specification from insulating grades.
capability
CNC Milling, Turning & Machining Capability
Great Plastics combines plastic-material supply with CNC machining. Your part geometry determines whether milling, turning or combined operations provide the better route.
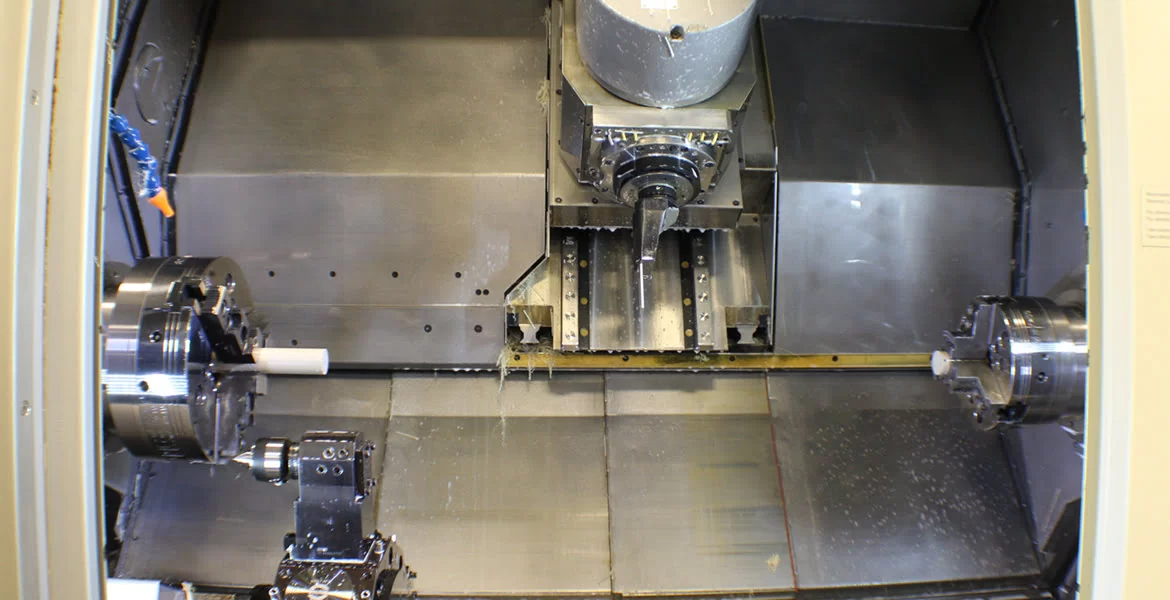
CNC Milling
Pockets, mounting faces, bolt patterns and intersecting holes in blocks and plates. Three-axis vertical machining provides a nominal envelope up to 1500 × 800 × 500 mm. Tool access and fixture clearance determine how much of that envelope your part can use.
CNC Turning
Seats, stepped bores, sleeves, grooves and threaded profiles from round stock. Nominal turning capacity is up to Ø431 × 990 mm. Long, thin walls need support to limit deflection. Chucking length and stock availability reduce the usable part size.
Combined Turning & Milling
Dual-spindle turn-mill equipment brings flats, radial holes and off-axis features onto turned parts. Fewer transfers can help preserve the relationship between the bore, outside diameter and secondary features. Feature access and tooling still determine the setup.
Machine envelopes are not guaranteed finished-part dimensions. Material, stock form, workholding and cutting access define the feasible size for your drawing. CNC Plastic Machining Capabilities
compatibility
Complex Features. Controlled Fits
Critical tolerances belong at the sealing, sliding and assembly interfaces. Feature-specific tolerances are agreed from your drawing, with the material and measurement conditions defined.
Sealing Faces & Concentric Bores
A seat profile, groove depth and bore-to-OD runout each control a different part of the fit. Thin sealing lips can move under clamping.
Dimensional acceptance:
Check the agreed features in the defined material and measurement conditions.
Operating fit:
Thermal expansion, moisture and creep can change clearances under heat and sustained load.
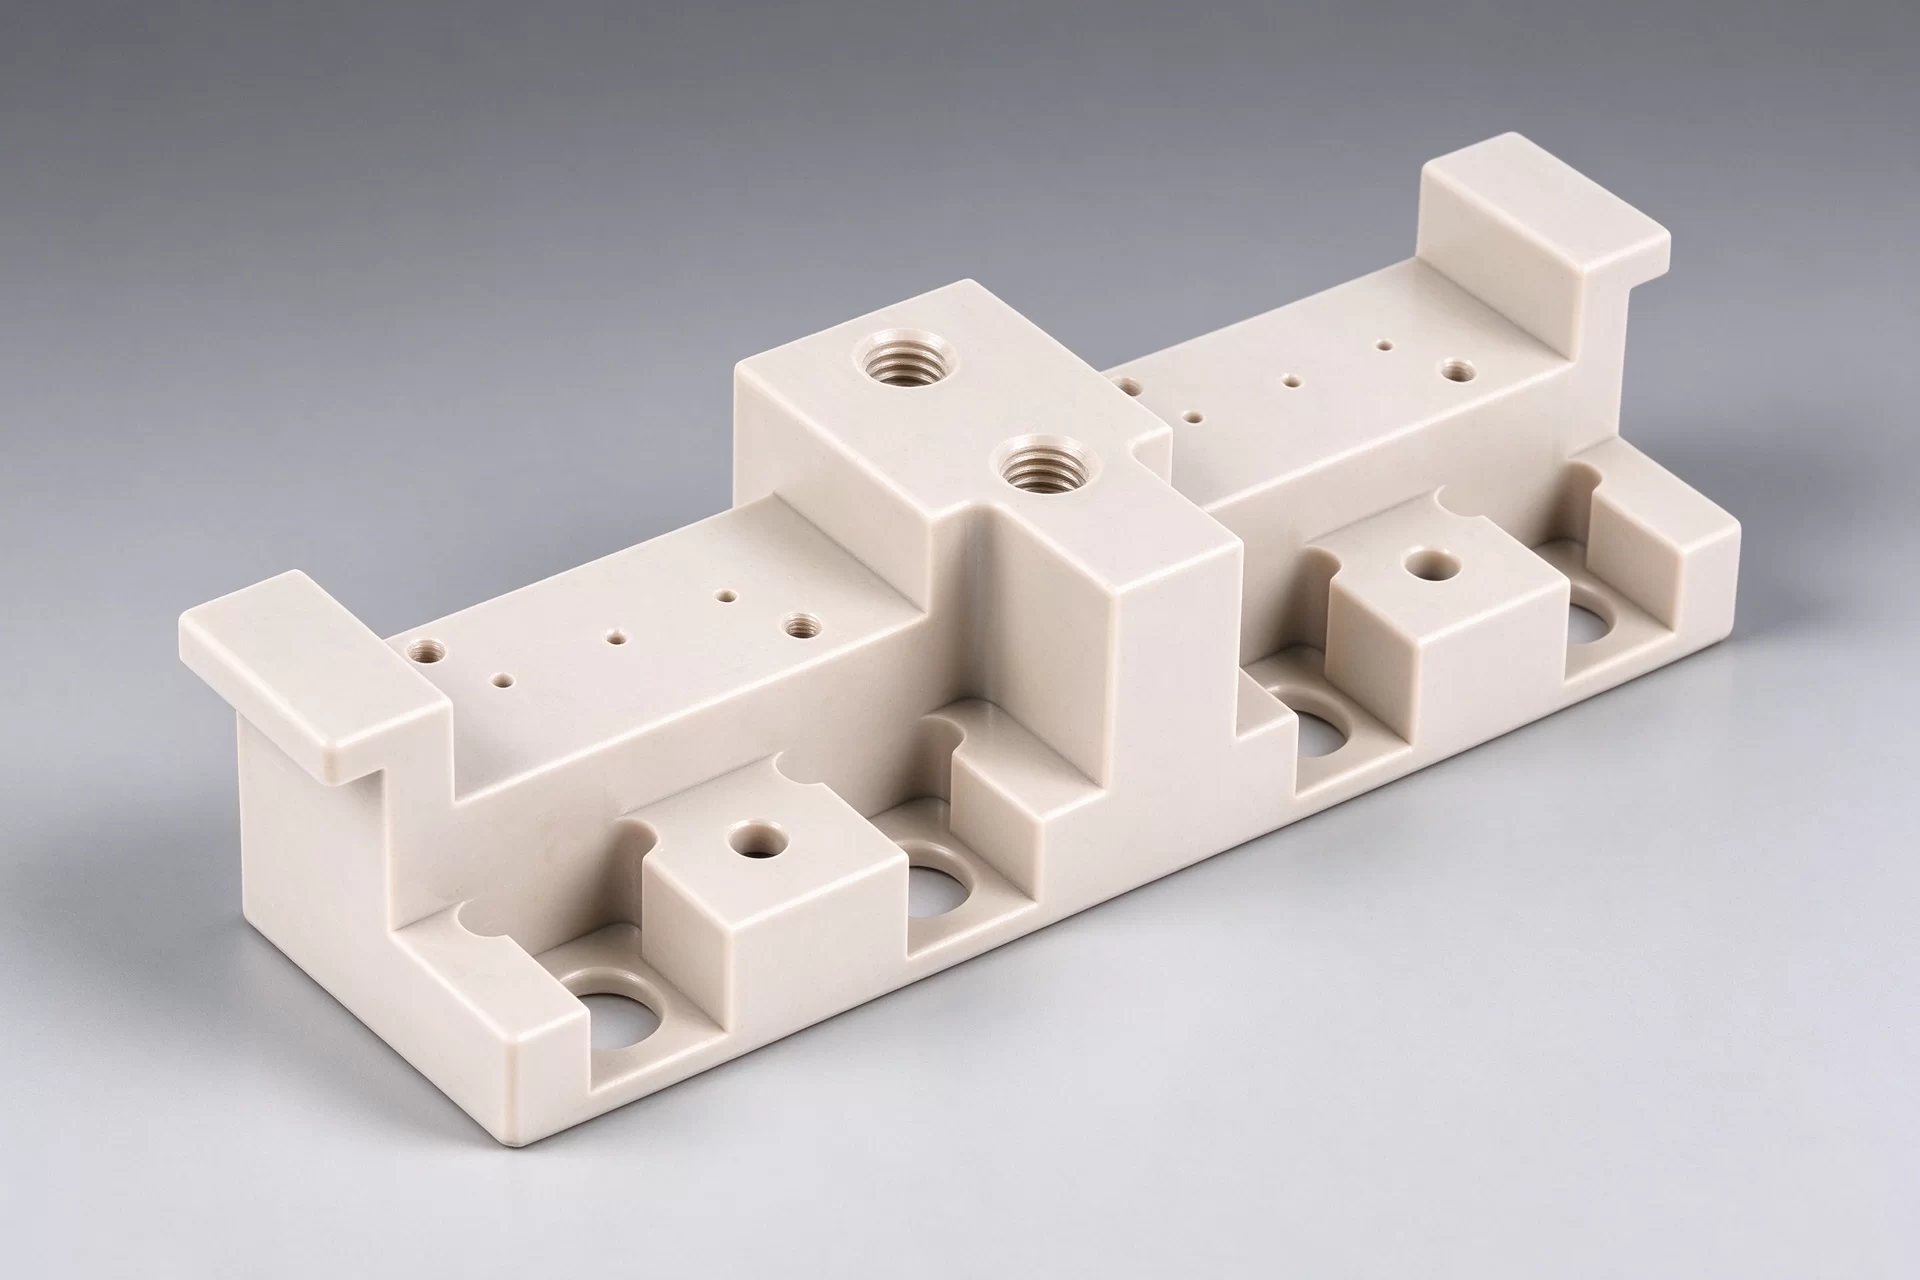
Mounting Holes & Ribbed Supports
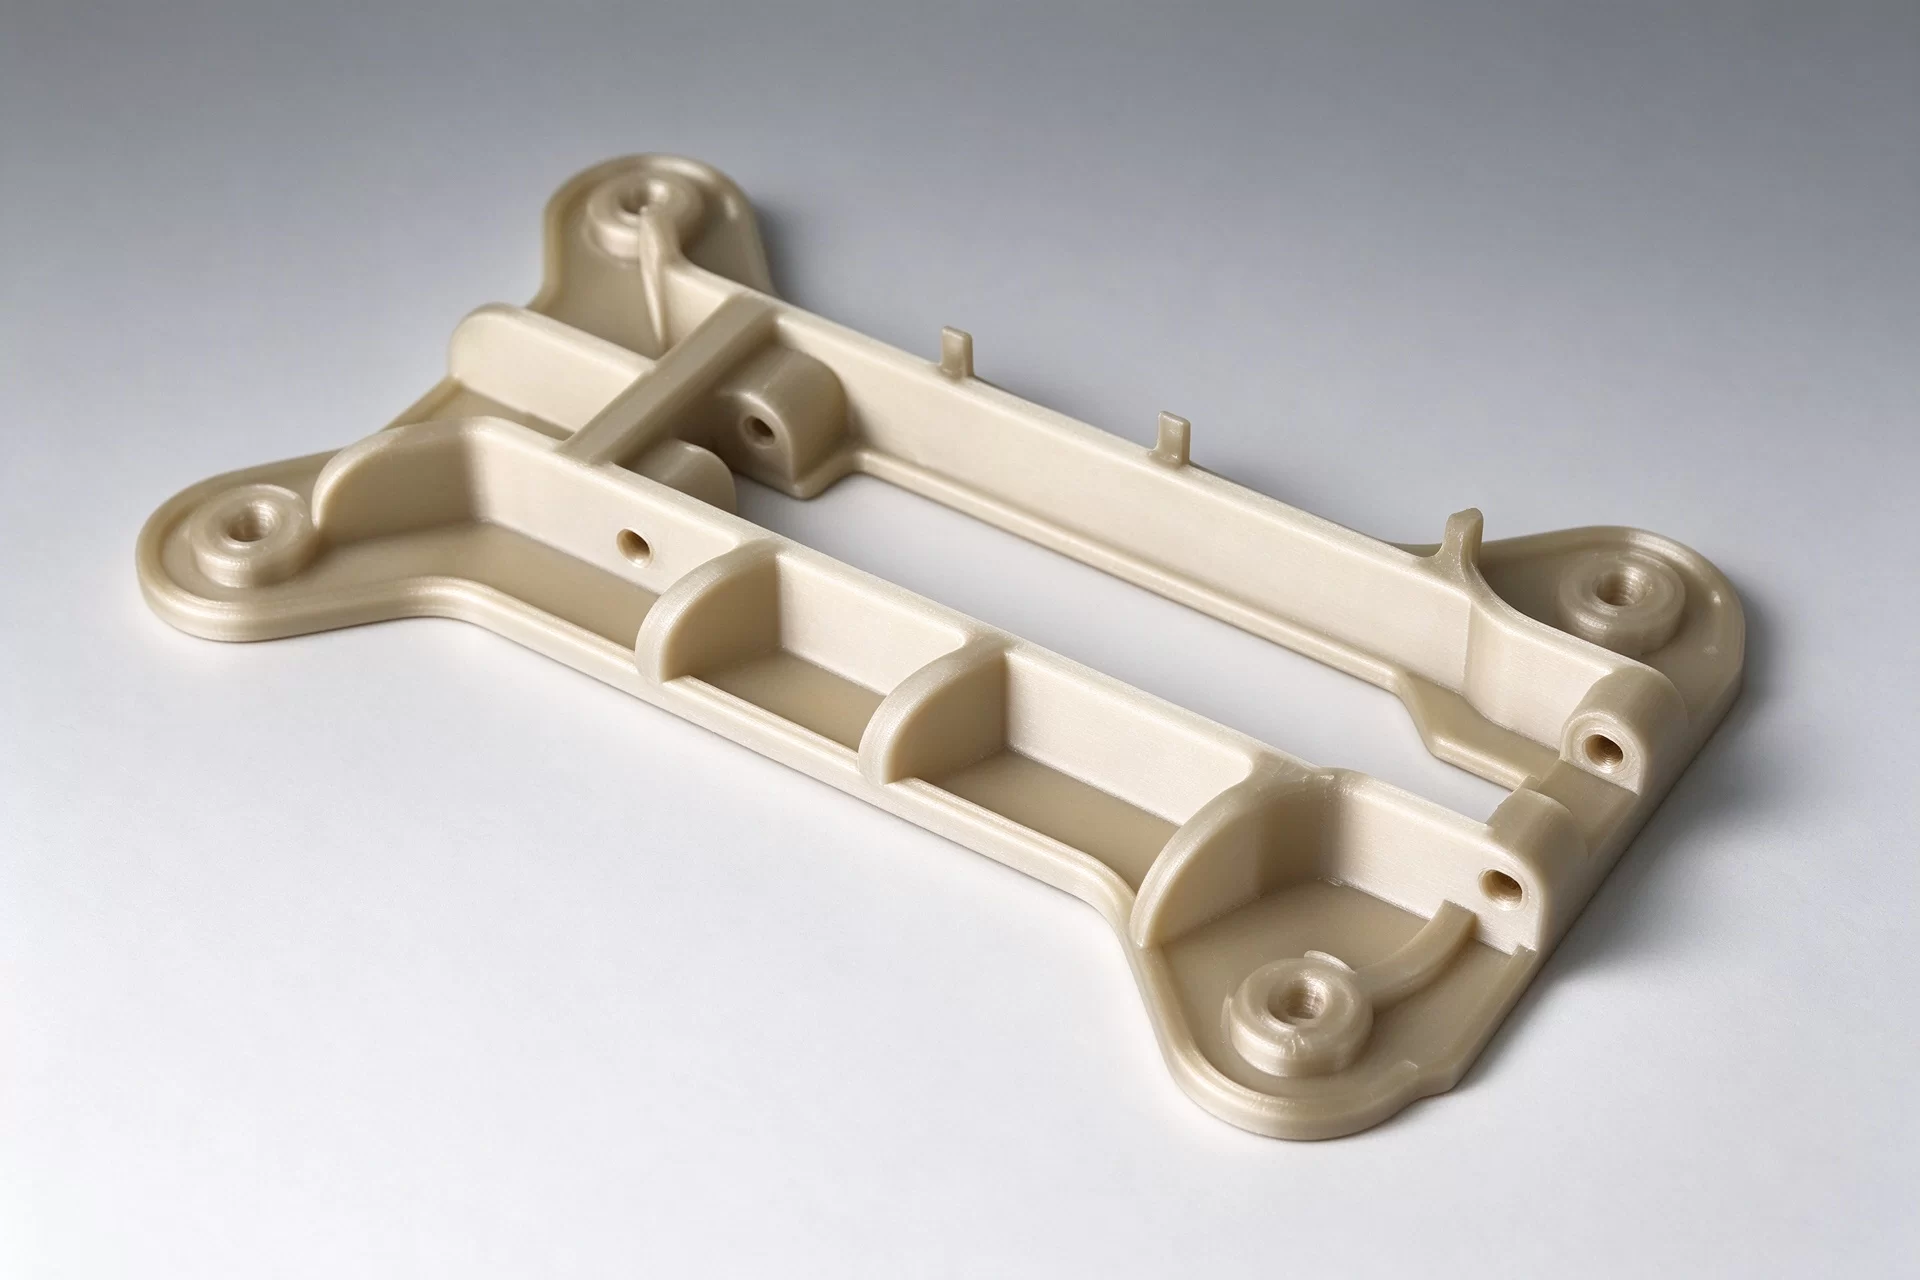
The representative bracket geometry combines mounting bores, ribs and recessed faces. Datum choice connects the hole pattern to the mating surface. Internal radii and tool reach constrain deep pockets; thin ribs need support during machining.
Windows & Slender Walls
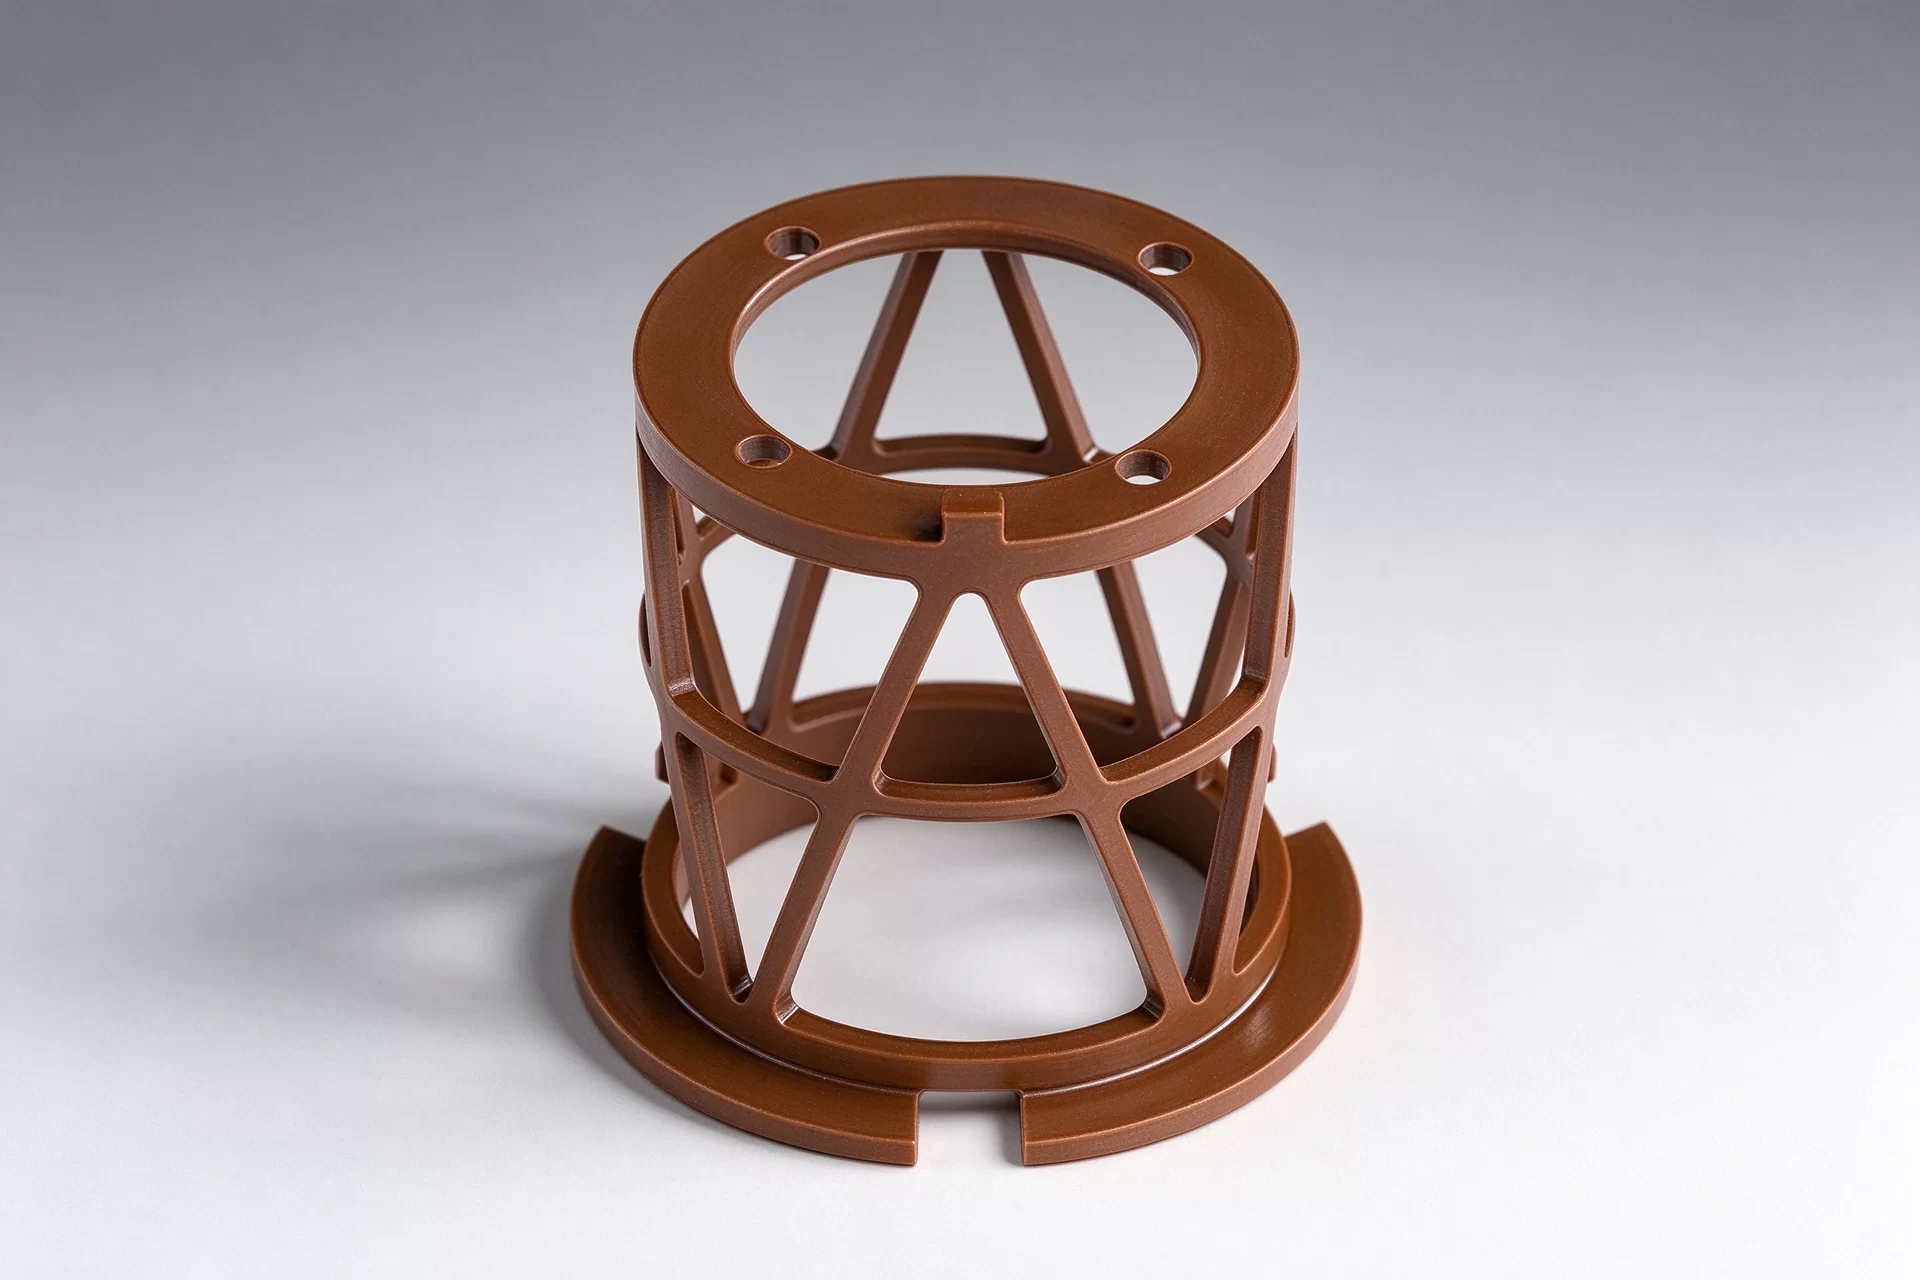
PI cage machining involves open windows, thin webs and flanged ends. Cutter access and machining sequence control wall deflection, while cross-drilled passages must allow burr removal. Enclosed features may require redesign.
Material Selection
Material Options for Your Operating Conditions
Material fit depends on chemical exposure, temperature, load, motion and electrical duty together. Match the exact grade to your service conditions; a polymer family name alone does not establish suitability.
| Material | Component fit | Grade choice & limits |
|---|---|---|
| PEEK | Valve seats, backup rings, bushings and connector bodies. | Unfilled, glass-filled, carbon-filled and bearing grades serve different duties. Fillers change stiffness, wear and electrical behavior. Strong oxidizers need specific compatibility evidence. |
| PPS | Fluid-contact parts, guides and dimensionally stable supports. | Unfilled, glass-filled, carbon-filled and wear-modified grades differ. Thin edges and notches need care. Chemical compatibility depends on the complete formulation and exposure conditions. |
| PEI | Electrical housings, pin carriers and dry-side supports. | Useful where stiffness and insulation matter. Fluid compatibility and stress cracking can limit exposed parts; specify the electrical grade. |
| PAI | Loaded bushings, thrust parts and wear components. | Moisture conditioning affects dimensions. Hot water, steam and amines need particular review. Specify the filler and conditioning state. |
| PI | Hot supports, insulating spacers and specialized wear parts. | Grade, atmosphere and contact conditions govern suitability. Moisture, hot-water exposure and fillers can change the working fit. |
Carbon-filled grades may be electrically conductive. A room-temperature clearance or chemical rating does not establish performance under heat, pressure and sustained load.
Services
Manufacturing Services for Energy Products
| Leverage the same speed, precision, and reliability in machining that you’re accustomed to at Great plastics but unlock advanced machining capabilities like tighter tolerances and volume pricing through our manufacturing network. Learn more→ |
|
 |
| Get affordable, high-quality molded parts and bridge tooling within days. With our free moldability consultation, the design and molding process is rapidly accelerated to save you time and money. Learn more→ |
|
|
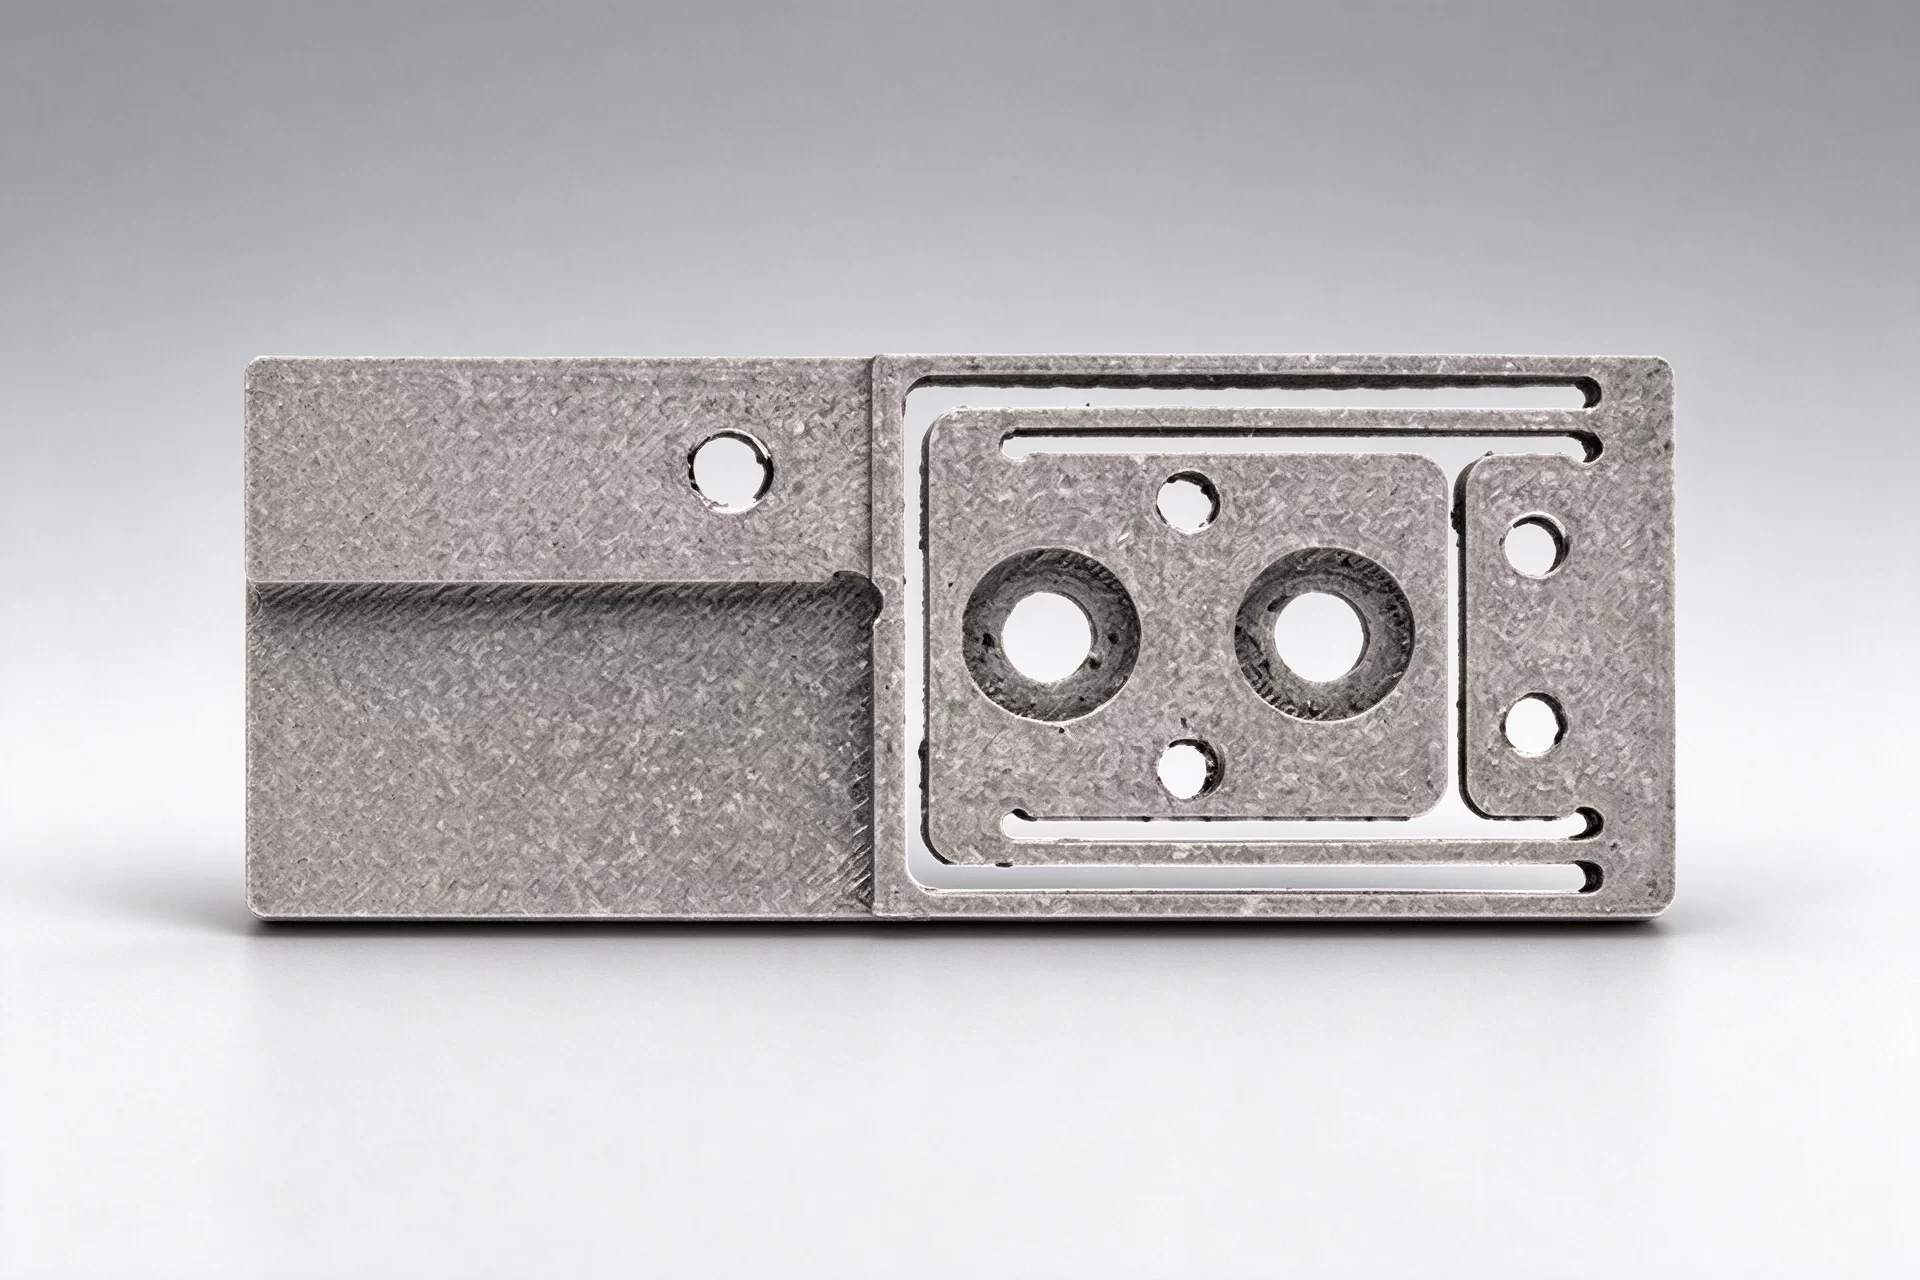
| Want quality parts and additive expertise at a single 3D printing source? Choose from fore different additive manufacturing technologies for cost-effective prototyping and highly precise, repeatable production parts. Learn more→ |
|
 |
How a Project Moves Forward
From Prototype to Repeat Production
Develop the part in its intended material, then carry the accepted geometry into production. Great Plastics supports prototypes, small batches and repeat orders for energy equipment components.
Prototype & Application Validation
Review the drawing, material and critical features. Test machined prototypes for fit and performance under actual operating conditions.
Small-Batch Production
Use the approved sample, drawing revision, material grade and key dimensions as production references.
Repeat Supply
Maintain the approved material, drawing and inspection requirements. Revalidate changes to geometry, fillers or operating conditions.
Buyer questions